Leave Your Message

Top 10 Injection Molding Part Design Companies in China

Choosing an Injection Molding Part Design company in China involves more than comparing tooling prices. A small design decision can affect thousands of production cycles. Consider a housing with thick screw bosses: material buildup can cause visible sink marks on the outer surface. Uneven walls can also increase cooling time and contribute to warpage. Details matter. This guide to the top 10 companies focuses on engineering capability, practical collaboration, and evidence buyers can verify.

In Plastic Part Design for Injection Molding, polymer engineering expert Robert A. Malloy explains how geometry, material selection, and processing interact. That perspective provides a useful foundation for evaluating design partners. A capable team should explain draft angles, rib thickness, gate placement, and realistic dimensional tolerances before tooling begins. For example, a snap-fit enclosure needs different design decisions than a glass-filled nylon bracket carrying repeated loads. Ask for documented design reviews, relevant project examples, and clear explanations of simulation assumptions. Request evidence. Attractive renderings alone reveal little about whether a part will eject reliably or meet assembly requirements.

China offers a broad supplier base, but company size does not automatically establish technical suitability. A smaller specialist may understand your application better than a larger general manufacturer. Even experienced teams can overlook resin shrinkage or underestimate the effect of a textured surface on draft requirements. No ranking eliminates that uncertainty. The companies considered here should therefore be assessed against your material, production volume, inspection requirements, and ownership terms. The strongest Injection Molding Part Design partner makes trade-offs visible and supports recommendations with measurable engineering evidence.
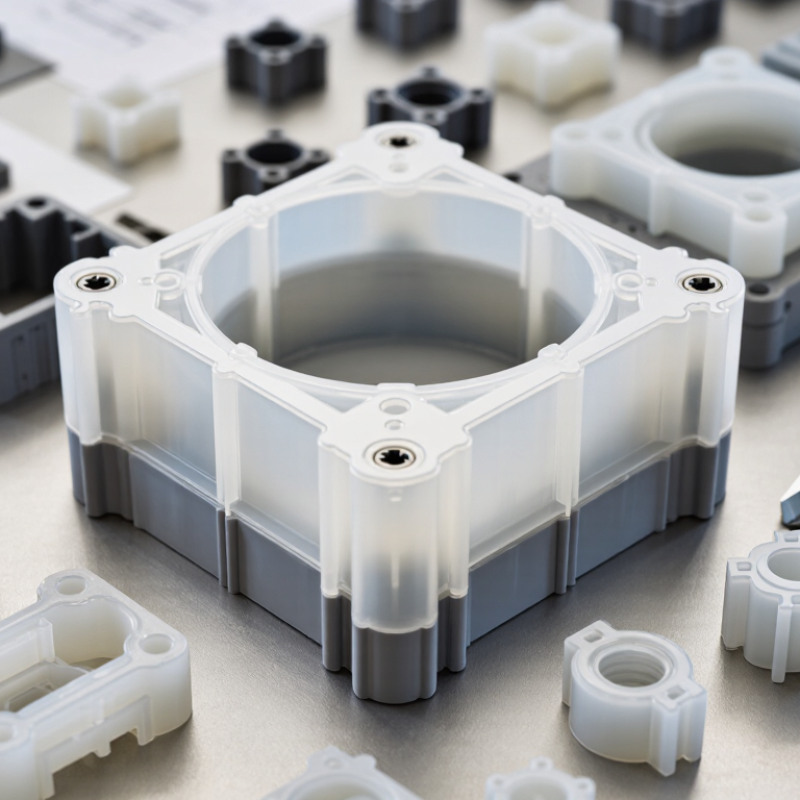
Top 10 Injection Molding Part Design Companies in China

Definition and Scope of Injection Molding Part Design

Injection molding part design turns a product concept into geometry that can be molded, assembled, and inspected consistently.

It covers material selection, wall thickness, draft angles, ribs, bosses, and dimensional tolerances. The part itself matters. Mold design is related, but focuses on the tooling that produces that part. When evaluating design companies in China, check whether their scope includes manufacturability reviews, engineering drawings, and prototype validation.

Consider a plastic enclosure with screw bosses and snap-fit clips.

Uneven walls can cause sink marks, while sharp internal corners can concentrate stress. Designers often start with relatively uniform walls and add radii where space permits. A draft angle around one degree may suit some smooth surfaces, but textured surfaces often need more.

Material changes everything. Shrinkage, moisture absorption, operating temperature, and chemical exposure influence dimensions and performance. A resin datasheet provides a starting point; testing must confirm suitability under actual service conditions.

The scope also includes reviewing gate locations, weld lines, ejection marks, and assembly access with the mold maker.

Simulation can flag filling risks, but its predictions depend on material data and processing assumptions. Some compromises remain uncomfortable: thicker ribs may improve stiffness while increasing visible surface defects. An early prototype can reveal assembly problems yet fail to reproduce molded shrinkage.

Clear deliverables should therefore include documented assumptions, critical dimensions, and a plan for checking initial molded samples.

Criteria for Evaluating Injection Molding Part Design Companies in China

Evaluating injection molding part design companies in China starts with evidence of engineering judgment. Request an anonymized design review for a component with ribs, bosses, and snap fits. Look for material-specific advice on wall thickness, draft angles, gate locations, and shrinkage. A capable team should explain how each decision affects appearance, strength, tooling complexity, and production cost. Ask for tradeoffs. A thinner wall may reduce cooling time but create filling problems along a long flow path.

Simulation reports deserve scrutiny because attractive flow plots alone reveal little about whether the underlying assumptions reflect your production conditions. Check the resin grade, processing assumptions, weld line locations, and predicted warpage. Ask how engineers compared predictions with actual molded samples and what changed after testing. Evidence matters. For dimensionally sensitive parts, request a measurement plan identifying critical features, inspection methods, and acceptance limits. Certificates can support supplier screening, but their scope and validity need verification.

Communication and revision control also deserve weight when comparing candidates for a top-ten shortlist. Confirm who approves design changes, owns CAD files, and maintains revision histories across engineering and tooling teams. Request a quotation separating design work, simulation, prototype iterations, and tooling support. A scoring sheet may initially overvalue fast replies; that deserves reconsideration when technical answers remain vague. Leave room to reassess. A slightly slower team may provide clearer risk assessments, although response delays still need agreed limits.

Top 10 Injection Molding Part Design Companies in China

Choosing candidates for a top 10 injection molding part design shortlist in China requires more than comparing polished product renderings. Strong teams explain how a part will fill, cool, shrink, and eject before tooling begins. Ask for anonymized design reviews showing wall thickness, draft angles, gate positions, and tolerance decisions. Details matter. A capable designer should explain why a deep rib could cause sink marks on a visible surface. Relevant project records provide stronger evidence than unsupported claims about rankings or production capacity.

Evaluate technical judgment through a small, clearly scoped design review. For example, submit a plastic enclosure with screw bosses, snap fits, and a textured exterior. Ask how the team would reduce thick sections while preserving fastening strength. Request material-specific recommendations, since polypropylene and glass-filled nylon behave differently during molding. Flow simulation can reveal potential weld lines and filling problems, but its assumptions still need checking against molding trials. Check the assumptions. A clean simulation image alone does not prove that a design will perform reliably.

Communication and documentation also deserve weight when comparing Chinese design partners. Look for revision histories, written acceptance criteria, and clear responsibility for engineering changes. An attractive quotation may omit prototype iterations or support during initial mold trials. That omission can make an apparently economical proposal harder to compare fairly. Some compromises remain uncomfortable: thinner walls may reduce material use while making filling more demanding. Ask each candidate to document those tradeoffs before approving the final part geometry.

Comparison of Design Capabilities, Materials, and Industry Expertise

Comparing ten injection molding part design companies in China requires more than checking polished CAD images. Look for documented design reviews covering wall thickness, draft angles, ribs, and gate placement. Details matter. For example, a 2 mm housing may need thinner ribs to reduce visible sink marks. Ask whether engineers provide moldflow analysis and explain its assumptions. Simulation helps, but trial molding can still reveal unexpected warpage. A detailed review of one sample part often reveals more than a lengthy capability presentation.

Material expertise should match the product’s operating conditions. A team experienced with polypropylene containers may need additional evidence before designing glass-filled nylon brackets. Ask how moisture absorption, fiber orientation, and shrinkage affect dimensions. For transparent polycarbonate covers, discuss gate marks, optical distortion, and cosmetic acceptance criteria. Industry experience also changes priorities. Consumer electronics often emphasize appearance and snap-fit assembly, while industrial equipment may prioritize chemical resistance and dimensional stability. Relevant evidence includes anonymized drawings, inspection reports, and documented design revisions. Portfolio photos alone provide limited proof.

Tips: Give every shortlisted company the same drawing, resin grade, annual volume, and critical dimensions. Compare their questions. Request a written explanation of proposed changes and their effect on tooling, assembly, and inspection. Be specific. An impressive proposal can still miss a difficult tolerance; that deserves another review. Ask who approves revisions and how unresolved risks appear in the project record.

Top 10 Injection Molding Part Design Companies in China - Comparison of Design Capabilities, Materials, and Industry Expertise

A company-neutral framework for comparing suppliers through ten injection-molded part design specialties.

The entries compare established design specialties, materials, and application requirements. They are not anonymous company profiles or a verified supplier ranking.
Part Design Specialty Design Capabilities to Evaluate Common Material Options Relevant Industry Expertise Key Engineering Considerations Evidence to Request
Consumer Electronics Enclosures Thin-wall housing design, snap-fit joints, screw bosses, rib design, cosmetic surface definition, and assembly clearance analysis. ABS, PC, and PC/ABS; flame-retardant grades where the application requires them. Consumer electronics, networking equipment, and handheld devices. Wall-thickness transitions affect sink and warpage. Draft, gate placement, and weld-line location influence appearance and mold release. DFM report, assembly tolerance analysis, resin grade specification, and approved cosmetic acceptance criteria.
Automotive Interior Components Trim attachment design, clip integration, textured surface design, dimensional control, and assembly interface development. PP, filled PP, ABS, and PC/ABS, selected according to mechanical, thermal, and appearance requirements. Automotive interiors, instrument-panel components, and cabin trim. Heat exposure, UV stability, odor, emissions, and flammability requirements vary by component and customer specification. Relevant automotive project examples, material qualification records, dimensional reports, and PPAP documentation when required.
Medical Device Housings and Components Assembly interface design, tolerance analysis, cleanability assessment, and design for the intended manufacturing and sterilization processes. Application-specific grades of PC, PP, ABS, and PPSU; selection depends on contact conditions and sterilization exposure. Diagnostic equipment, medical instrument housings, and selected disposable device components. Biocompatibility depends on the finished device and its contact conditions. Sterilization can alter material strength, dimensions, and appearance. Material traceability, documented design controls, sterilization compatibility evidence, and applicable biological evaluation documentation.
Electrical Connectors and Insulating Parts Contact retention features, fine-feature design, insert positioning, creepage and clearance layout, and dimensional tolerance analysis. PBT, PA66, and LCP; glass-filled or flame-retardant grades as required. Electrical connectors, industrial controls, power electronics, and electrical equipment. Moisture absorption, processing shrinkage, dielectric performance, and heat resistance affect material selection and dimensional stability. Resin data sheets, electrical property data, dimensional inspection results, and applicable flame classification documentation.
Precision Gears and Sliding Components Gear geometry, bearing and shaft interfaces, tolerance allocation, wear surface design, and shrinkage compensation. POM, PA, and PBT; lubricated or reinforced grades where justified by the application. Small mechanisms, appliances, office equipment, and industrial motion assemblies. Load, speed, lubrication, moisture, and temperature influence wear and dimensional behavior. Reinforcement can introduce directional shrinkage. Gear inspection results, wear or endurance testing, operating-condition assumptions, and critical-dimension capability data.
Transparent Covers and Optical Components Optical surface definition, gate positioning, wall-thickness control, flow analysis, and cosmetic defect prevention. PMMA and PC; optical grades where light transmission and optical quality are critical. Lighting, display windows, instrument covers, and optical devices. Residual stress, flow marks, contamination, and weld lines can affect optical performance. PMMA and PC have different impact and scratch-resistance characteristics. Transmission and haze results where applicable, surface specifications, optical inspection criteria, and molding trial reports.
Food-Contact Containers and Closures Closure fit, sealing features, nesting geometry, thin-wall design, and living hinges where the chosen material supports them. Suitable food-contact grades of PP and PE, including HDPE and LDPE. Food packaging, beverage closures, kitchenware, and reusable containers. Food-contact suitability depends on the complete formulation, intended food type, temperature, duration of contact, and destination-market requirements. Food-contact declarations, applicable migration test results, seal or leak testing, and hinge-cycle testing where relevant.
Soft-Touch and Sealing Components Overmold interface design, mechanical interlocks, seal geometry, compression control, and two-shot molding feasibility assessment. TPE and TPU, paired with compatible rigid substrates such as PP, ABS, or PC as appropriate. Handheld products, appliance seals, grips, and protective components. Adhesion is specific to the elastomer grade and substrate combination. Hardness, compression set, chemical exposure, and temperature affect service performance. Material compatibility guidance, adhesion testing, leak testing, and compression-set or durability data matched to the application.
High-Temperature Engineering Components Load-bearing geometry, thermal expansion analysis, insert interfaces, reinforcement orientation review, and high-temperature tolerance assessment. PPS, PEEK, and PEI; reinforced grades where required by structural or dimensional needs. Industrial equipment, electrical systems, and selected automotive or aerospace applications. Long-term temperature exposure, creep, chemical resistance, and processing requirements must be evaluated for the specific resin grade and operating conditions. Thermal aging data, creep data, chemical compatibility evidence, process capability records, and application-specific validation results.
Large Housings and Appliance Panels Rib layout, boss reinforcement, gate strategy, cooling layout review, warpage analysis, and assembly datum planning. PP, ABS, PC/ABS, and glass-filled PP, depending on stiffness, appearance, and service conditions. Home appliances, equipment housings, and industrial enclosures. Large projected areas increase clamp-force requirements. Uneven cooling, wall-thickness variation, and directional shrinkage can cause distortion. Filling and warpage analysis, machine and mold feasibility assessment, dimensional inspection reports, and assembly-fit trial results.

Material selection: Polymer names describe material families. Final performance depends on the exact grade, additives, processing conditions, part geometry, and service environment.

Supplier comparison: Use these criteria when evaluating injection molding part design companies in China. Confirm each supplier’s capabilities through documented project evidence, engineering reviews, and relevant validation results.

Standards context: ISO 20457 addresses tolerances and acceptance conditions for plastic molded parts. ISO 10993-1 provides a framework for biological evaluation of medical devices. UL 94 addresses flammability testing of plastic materials. Their applicability depends on the product and its requirements.

How to Select an Injection Molding Part Design Partner

Choosing among China’s injection molding part design companies requires more than comparing attractive CAD renderings. Ask for anonymized examples showing how a design changed after mold trials. Look for documented decisions about wall thickness, draft angles, gate placement, and ejector marks. Details matter. For a small ABS enclosure, ask how the team would reduce sink marks around internal screw bosses. A capable partner should explain material behavior and tooling constraints before committing to dimensions or delivery dates. Request a sample DFM report, including identified risks and proposed corrections.

Tips: Share your resin grade, annual volume, cosmetic requirements, and critical dimensions before requesting quotations. Compare identical deliverables across suppliers. Ask who owns the CAD files and whether mold-trial revisions are included. Check revision limits.

Simulation reports can support decisions, but they cannot replace physical trials and measured inspection results. Ask whether the designer joins tool reviews and evaluates first-shot samples with the moldmaker. For a snap-fit lid, request an agreed test method for assembly force and repeated opening. A lower design fee may exclude tolerance analysis, prototype testing, or production troubleshooting. An early prototype may feel acceptable while still hiding uneven shrinkage; that uncertainty deserves attention. Put acceptance criteria, communication responsibilities, and revision approval procedures in writing before work begins.

Selecting an Injection Molding Part Design Partner in China: Material Shrinkage Matters

Material shrinkage affects tooling dimensions, dimensional accuracy, and assembly fit. These typical shrinkage ranges provide a practical starting point for evaluating a design partner’s understanding of material selection and mold compensation.

Typical molding shrinkage ranges: ABS 0.4–0.9%; PC 0.5–0.7%; PP 1.0–2.5%; HDPE 1.5–3.0%; POM 1.8–2.5%.

How to use this chart: Ask prospective design partners how they select shrinkage allowances, assess warpage, and validate critical dimensions. For example, a 100 mm dimension with 2% shrinkage involves approximately 2 mm of dimensional change. A capable partner should use the selected resin grade’s data and processing conditions to determine the actual tooling allowance.

Data context: The bars show representative typical ranges for unfilled materials, not guaranteed limits or company performance scores. Actual shrinkage depends on resin grade, flow direction, part geometry, and molding conditions. Reference: polymer molding shrinkage reference. Confirm final values against the selected material supplier’s technical datasheet.