Leave Your Message

Top Injection Molding Companies in the World?

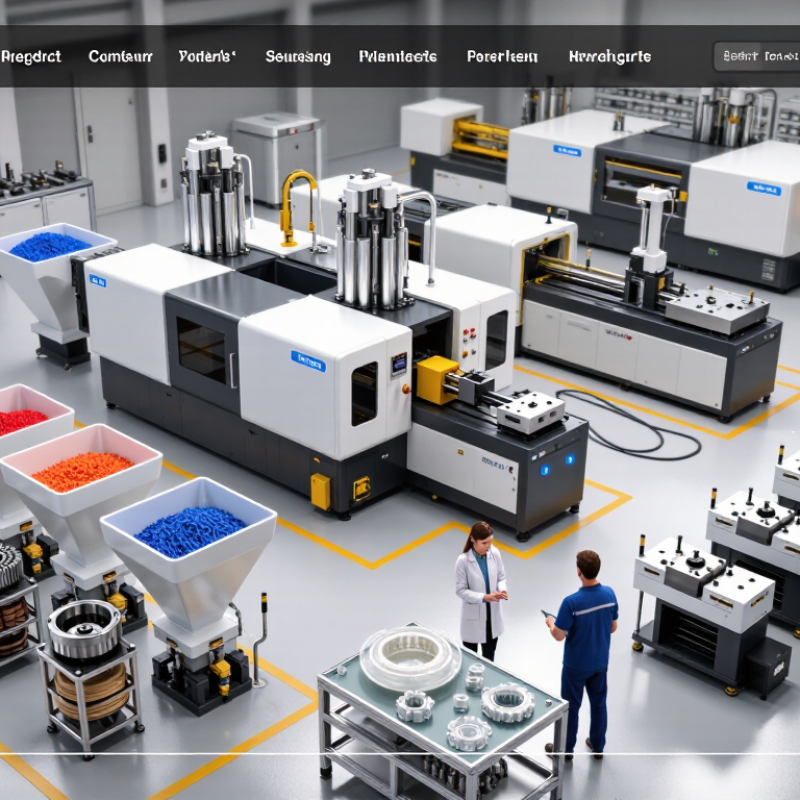
Choosing among the world’s leading Injection Molding Companies takes more than comparing factory size or annual output. Buyers need dependable part quality, suitable materials, and production capacity that matches real demand. A polished website is not proof of a capable plant. The evidence is in process controls, tooling experience, inspection records, and consistent delivery.

John Bozzelli, an injection molding specialist and educator, is associated with the phrase, “Scientific molding is a process, not a machine.” The idea matters. A modern press cannot compensate for unstable settings, weak mold design, or poor communication between engineering and production. Small details count: a marked inspection station, a clean tool-storage area, or a documented change to a resin specification can reveal how a supplier manages risk.

This overview examines companies through practical criteria, including technical expertise, quality systems, automation, material options, and regional support. It also considers how well suppliers handle prototyping, complex geometries, and high-volume programs. No ranking can fit every buyer. A medical-device project and an automotive component have different priorities, and published claims do not always tell the full story. That limitation deserves attention. Use this guide as a starting point, then verify capabilities, certifications, references, and sample parts directly with each shortlisted manufacturer.
Top Injection Molding Companies in the World?

Injection Molding Basics: 4 Stages from Melting to Part Ejection

Injection molding turns plastic pellets into repeatable parts through four connected stages. In the barrel, heat and screw friction soften pellets into a flowing melt. The screw then pushes a measured shot through the nozzle and into a closed mold. Fast filling helps, but excessive speed can trap air or damage heat-sensitive resin.

Packing pressure replaces material as the melt shrinks. Cooling hardens the part against the mold walls; small differences in wall thickness can leave uneven shrinkage or a warped edge. Ejector pins then push the cooled part free. The cycle sounds tidy. Real parts can be less forgiving. It is easy to focus on filling speed and underestimate cooling time, which often shapes both cycle time and part quality.

Grand View Research’s 2024 injection-molded plastics market report estimated a global market value of US$330.1 billion in 2023, with a projected 4.8% compound annual growth rate through 2030. That estimate signals the process’s industrial scale, not a guarantee of any single factory’s output.

For a molded component, check the four stages together: melt consistency, filling pattern, cooling balance, and clean ejection. A smooth surface can still hide internal stress.
How to Rank Global Companies: Revenue, Production Capacity, and Reach

A credible ranking of global injection molding companies should compare more than headline revenue. Revenue shows commercial scale, but it may include packaging, assembly, or other services beyond molding. Where possible, use audited reports and separate molding income from broader business activities. Convert currencies using the same year and exchange-rate method. Numbers need context.

Production capacity is harder to measure. A useful assessment considers press count, clamping-force range, annual output, facility locations, and utilization. A factory with many machines may still have limited available capacity during peak seasons. Ask whether reported figures cover installed equipment or actual production. Resin type, part size, cycle time, and tooling needs also affect what a company can make. These details are often missing, which makes comparisons imperfect.

Reach reflects how reliably a supplier can serve customers across regions. Look for operating plants, local technical support, logistics options, and experience managing consistent quality between sites. A broad network can reduce shipping time, yet distant facilities do not automatically mean responsive service. Rankings should state their data sources, reporting dates, and scoring weights. Without that transparency, a precise-looking list may tell only part of the story.

Leading Machine Makers: Haitian, ENGEL, ARBURG, Milacron, and Sumitomo Demag

The global injection molding machine market includes manufacturers with different strengths, rather than one universal leader. Some focus on high-volume production and competitive pricing. Others emphasize electric precision, process control, or flexible machine configurations. Buyers should compare clamp force, shot size, energy use, and local service support against the parts they actually make.

A machine’s reputation matters, but so does the technician who can reach a factory before a production line sits idle. In practice, mold trials reveal details that brochures cannot: filling consistency, cycle stability, and how easily operators adjust settings. A small variation in material temperature can change the result. That matters.

Leading suppliers often serve distinct needs across packaging, automotive, medical, and general manufacturing. Yet these categories overlap, and a premium machine may be unnecessary for a simple, stable part. Conversely, a low purchase price can become costly when maintenance access or spare parts are limited. I would not rank manufacturers without knowing the mold, resin, annual volume, and plant conditions. Even careful comparisons miss something: real production behavior is not always predictable from a showroom test.

Press Technology Compared: Clamping Forces from Under 100 to Over 10,000 Tonnes

Clamping force is one of the clearest ways to compare injection molding presses, but a larger rating does not automatically mean better production. Machines below 100 tonnes often suit small, precise parts such as clips, caps, and compact housings. Their smaller molds can be easier to change and may use less energy per cycle. Still, limited platen space can rule out a mold that seems light enough.

Mid-range presses handle many everyday components, from appliance panels to automotive fittings. The required force depends partly on the projected area of the part and the pressure inside the mold. A wide, thin component may need more clamping force than a compact, thick one. Mold design, resin behavior, and process settings matter too. Real shop-floor conditions can be messier than a calculator suggests.

At the other end, presses exceeding 10,000 tonnes are built for very large parts, including substantial vehicle or infrastructure components. Their size brings practical demands: heavy molds, ample floor space, and careful material handling. A company’s press range can indicate the projects it supports, but it cannot prove consistent quality by itself. Ask for machine specifications, available mold dimensions, and relevant production experience. The tonne rating is useful. It is not the whole story.

Top Injection Molding Companies in the World? — Press Technology Compared: Clamping Forces from Under 100 to Over 10,000 Tonnes
Nominal Clamping-Force Band Press Technologies Commonly Used Typical Strengths Common Applications Important Considerations
Under 10 metric tonnes-force Micro injection presses; compact all-electric or hydraulic machines Small footprint, precise control, and suitability for very small shot sizes Micro components, small connectors, medical and electronic parts Part size and shot capacity are limited; mold design and process control are especially important.
10 to under 100 metric tonnes-force Small toggle, hydraulic, and all-electric presses Compact tooling and efficient production of small parts; electric drives can provide repeatable motion control Small housings, closures, consumer components, and precision parts Required force depends on projected part area, cavity pressure, material, and mold layout—not part weight alone.
100 to under 1,000 metric tonnes-force Toggle, direct-hydraulic, hybrid, and all-electric presses Broad equipment choice and flexibility across many mold sizes and production requirements Appliance components, packaging, automotive interior parts, and general industrial products Machine selection also depends on shot capacity, platen dimensions, tie-bar spacing, and injection requirements.
1,000 to under 5,000 metric tonnes-force Large hydraulic, hybrid, and two-platen presses Accommodate large molds and high projected-area parts; two-platen layouts can reduce machine length for a given mold size Large automotive parts, pallets, bins, and appliance panels Factory floor loading, mold handling, energy demand, and safe access become major planning factors.
5,000 to 10,000 metric tonnes-force Very large hydraulic or two-platen presses Provide the high clamp force needed for large-area molds and demanding production applications Large containers, structural parts, and oversized automotive components Installation may require substantial foundations, specialized transport, and large supporting infrastructure.
Over 10,000 metric tonnes-force Specialized ultra-large hydraulic or multi-platen press systems Designed for unusually large molds, projected areas, or specialized production needs Very large structural and industrial molded components These are specialized installations; availability, configuration, and practical limits vary by application.
Clamping force is expressed in metric tonnes-force. The bands are indicative, not universal product categories: machine ranges overlap, and a suitable press must be selected using the mold, material, projected area, cavity pressure, shot size, and process requirements.

Key Markets for Global Suppliers: Automotive, Packaging, Medical, and Electronics

Global injection molding suppliers serve industries with very different priorities. In automotive, parts may include dashboard housings, clips, and under-hood components. Buyers look for repeatable dimensions, durable materials, and stable production across large runs. A tiny change in wall thickness can affect fit or cooling time. That detail is easy to underestimate.

Packaging favors speed and consistent output. Thin-wall tubs, caps, and closures often need carefully balanced mold cooling and material flow. Medical manufacturing places greater weight on controlled processes, traceability, and documented quality checks. Tooling changes may require careful review, especially when parts contact patients or support clinical equipment. Small defects matter.

Electronics suppliers produce items such as connector bodies, switches, and protective enclosures. These parts may need tight tolerances, heat resistance, or precise features for assembly. A supplier’s practical fit depends on its engineering support, inspection methods, material knowledge, and ability to manage production volumes. Low unit prices can be tempting, but they do not show the full cost of delays or inconsistent parts. No process is flawless. Buyers should also ask how problems are recorded and corrected; a polished capability sheet cannot answer every question.

Key Markets for Injection Molding Suppliers

European plastics demand by application, 2022 (% of total)

Packaging is the largest separately reported application in this regional dataset. “Other applications” aggregates several sectors; medical applications are not reported as a separate category. These figures describe plastics demand, not injection molding alone, and should be treated as market context rather than a global injection-molding market share.

Source: PlasticsEurope, Plastics – the Fast Facts 2023 (2022 European demand by application).